1-805-484-2992
Quotes - Engineering - SalesA plate pack with no gaskets and nothing to retighten
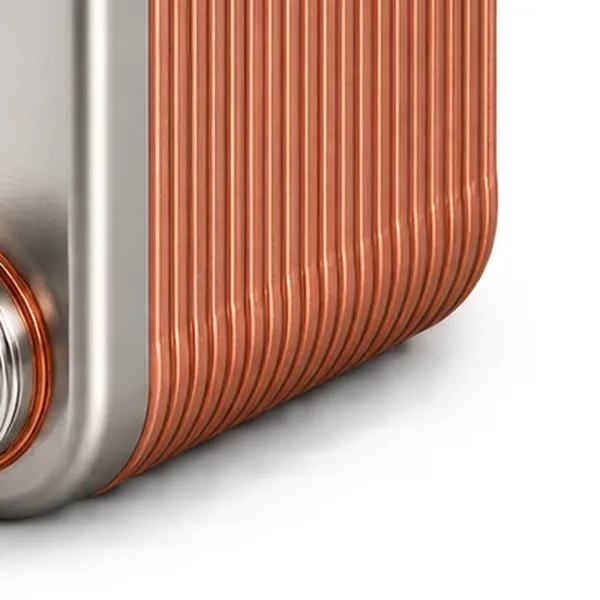
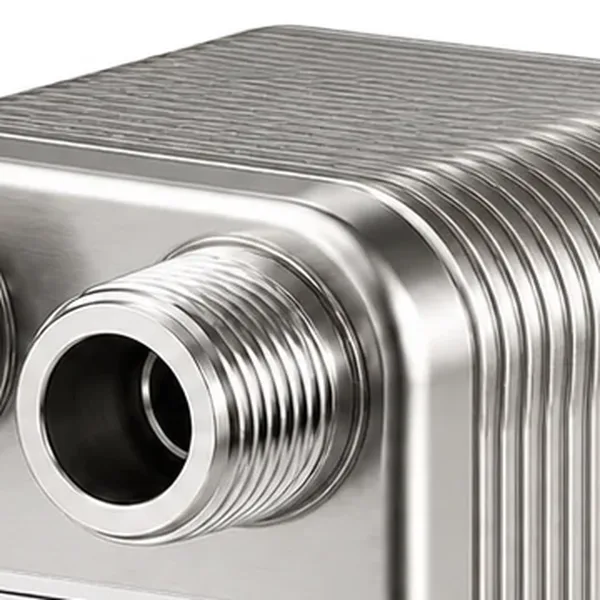
A brazed plate heat exchanger is a stack of corrugated 316L plates, each turned 180 degrees from the one below, with a thin foil of filler metal between them. The stack is heated under vacuum, the filler melts, and every contact point between plates becomes a brazed joint. The result is one solid block: no gaskets, no tie bolts, no frame, and a pressure rating of 435–650 psig (30–45 bar) from a compact block. The two fluids run in alternate channels 1–3 mm wide, in counterflow, with the corrugations driving turbulence at low velocity.
In stainless the plates are always the easy part. The decision that matters is the filler. Copper is the standard braze and suits clean water, glycol, oils and the HFC and HFO refrigerants. Nickel filler replaces it wherever copper is attacked or contaminates: ammonia, deionized water, some process chemicals. An iron-based stainless filler leaves no copper and no nickel-alloy braze in the wetted path, for duties where the product side must see only stainless.
This construction suits engineers who need a lot of surface in little space at high pressure and are working with clean, low-viscosity fluids: refrigerant evaporators and condensers, oil coolers, glycol loops, commercial hydronic isolation, process water cooling, and transcritical CO2 gas coolers rated to about 2,030 psig (140 bar). It does not suit fibrous or particulate streams, and it cannot be opened for cleaning, so the fluid chemistry has to be right before the unit is brazed, not after. Where a standard brazed plate model from a broader catalog fits the duty, the brazed plate heat exchanger range at SWEPHeatExchangers.com is a good place to compare sizes.
Plates are 316L on every brazed unit we supply; the filler is copper for clean water and glycol, nickel for ammonia and deionized water, and stainless where neither may touch the fluid. The Material & Construction page compares the grades.
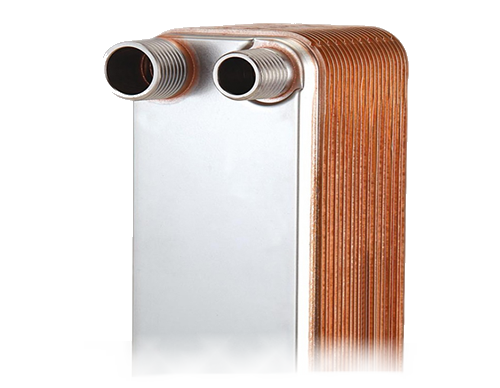
Several times the pressure rating of a gasketed plate unit, in a much smaller footprint, with a braze filler chosen for the fluid rather than taken on default.
Copper, nickel or all-stainless braze on 316L plates; -320 to 400°F.
Why brazed, in stainless
- 435–650 psig standard; CO2 designs to 2,030 psig
- No gaskets to age, harden or set a temperature limit
- Full counterflow with 2–5°F approach on liquid duties
- Envelope of -320 to 400°F covers cryogenic to steam
- One brazed block, no frame, no bolts, no gasket leak paths
Why the filler decides it
- Copper braze: water, glycol, oil, HFC and HFO refrigerants
- Nickel braze: ammonia, deionized water, copper-sensitive fluids
- All-stainless braze: no copper or nickel-alloy braze wetted
- Double-wall plates vent a leak for potable water codes
- Dual-circuit builds run two circuits on one common side
What you specify
Standard brazed plate build
The figures below are the common build we quote; higher ratings, special ports and dual circuits are to order.
| Feature | Standard build |
| Plate material | 316L stainless, dual-certified 316/316L |
| Braze filler | Copper standard; nickel or iron-based stainless filler to order |
| Design pressure | 435–650 psig (30–45 bar); to about 2,030 psig (140 bar) for transcritical CO2 |
| Design temperature | -320 to 400°F typical envelope |
| Channel gap | 1–3 mm; clean, low-viscosity fluids only |
| Flow arrangement | True counterflow, single pass; parallel flow or two pass to order |
| Connections | Threaded, sweat, flanged or weld-stub ports; cover plates on larger units |
| Leak-protection options | Double-wall plates with a vented gap; dual-circuit on one common side |
| Testing and documentation | Helium or air leak test and pressure test; MTRs and code stamp as specified |
Choosing a brazed plate unit in stainless
Where brazed beats gasketed and shell-and-tube
A gasketed plate frame is usually rated 150 psig and its elastomer sets the temperture ceiling at 230–350°F depending on the compound. A brazed unit has no elastomer, so the pressure and temperature limits are those of the plate and the braze. On refrigerant duty that difference is the whole case: a condenser at 300 psig saturation pressure, or a CO2 gas cooler running well above 1,000 psig, is beyond a gasketed frame and needs brazed, welded or shell-and-tube construction.
Against a shell-and-tube of the same duty the brazed unit holds a fraction of the volume and charge, which matters on refrigerant and costly thermal fluids. What it gives up is access. You can backflush it and chemically clean it, but you cannot open it.
Picking the braze filler
Copper is the default filler because it wets stainless well, forms a ductile joint, and costs least. It fails on ammonia, which forms copper-ammonia complexes and strips the joint, and on deionized or ultrapure water, which leaches copper and both corrodes the joint and contaminates the water. Those two duties take nickel filler. Nickel brazes harder and usually carries a slightly lower pressure rating, and the lead time and price are higher.
Where the process side cannot tolerate copper or a nickel-alloy braze in contact, the iron-based stainless filler makes the wetted path all stainless. Pick it for high-purity and food-adjacent duties; it does not raise the chloride limit, which stays that of the 316L plate.
- Copper: clean water, glycol, oils, HFC and HFO refrigerants
- Nickel: ammonia, deionized water, fluids that leach copper
- Stainless filler: no copper or nickel-alloy braze wetted
- Double wall on any filler where two fluids may not meet
Grade choice: 316L plates and what they will not do
Every brazed unit we supply uses 316L plates, thin enough to form in a press, so the plate grade is not the decision the way it is on a shell-and-tube. The limit to remember is chlorides. A 316L plate typically tolerates about 1,000 ppm chloride in clean, cool, near-neutral water, but the brazed joint is a crevice by nature, and the plate is thin enough that one pit is a through-wall leak. So we prefer water-side chloride under about 200 ppm and accept 200–1,000 ppm only on cool, clean, treated water after review; above that, or hot chloride water, is a duty for a plate-and-frame with titanium plates or a shell-and-tube in duplex, not a brazed unit that nobody can inspect.
The common mistake
The failures we see are almost never thermal. They are a copper-brazed unit put on ammonia or deionized water because the buyer specified the plate grade and never asked about the filler, or a brazed unit on dirty water with no strainer, plugged in a season because a 1–3 mm channel will not pass what a 3/4 in. tube will. Specify the filler by the fluid, strain any open loop, and keep brazed units off streams with fibers, scale or solids.
Before you choose a brazed plate
No. The plate stack is one brazed block, so an internal leak between channels is the end of the unit. That is the reason to get the filler and the water chemistry right at selection, to fit strainers, and to specify a double-wall version where a leak into a potable or product stream would be unacceptable. A replacement is usually a same-port-pattern swap.
Brazed units trade pressure drop for surface. On a liquid-to-liquid duty we usually design for 5–10 psi per side; pushing to 15 psi buys a smaller unit but higher pump power. Tell us the pump head available and we select plate count and channel pattern around it, not the smallest unit that meets the duty.
For clean water, glycol, oils and refrigerants, usually yes. For water above about 200 ppm chloride that is not cool, clean and treated, hot chloride water, or acidic process streams, no grade of brazed plate is the right answer, because the plates are thin and the joints are crevices. Those duties go to a gasketed plate-and-frame in titanium or a shell-and-tube in duplex or 6-moly, and we will say so on the quote.
Any open or once-through water loop needs a fine-mesh strainer upstream, and a closed glycol or chilled water loop should be flushed clean before the unit is cut in. The channel gap of 1–3 mm plugs on scale, weld slag and pipe-dope string that a shell-and-tube would pass without notice. Fouled brazed units are backflushed or chemically cleaned in place.
Dual-circuit puts two independent refrigerant or glycol circuits against one common water side, so a two-compressor chiller or a redundant cooling loop uses one exchanger. Double-wall inserts a second plate with a vented gap between the two fluids, so a plate failure drips to the outside instead of mixing streams; it is the construction potable water codes often call for and it costs some surface.
Related
Brazed Plate
All-Stainless
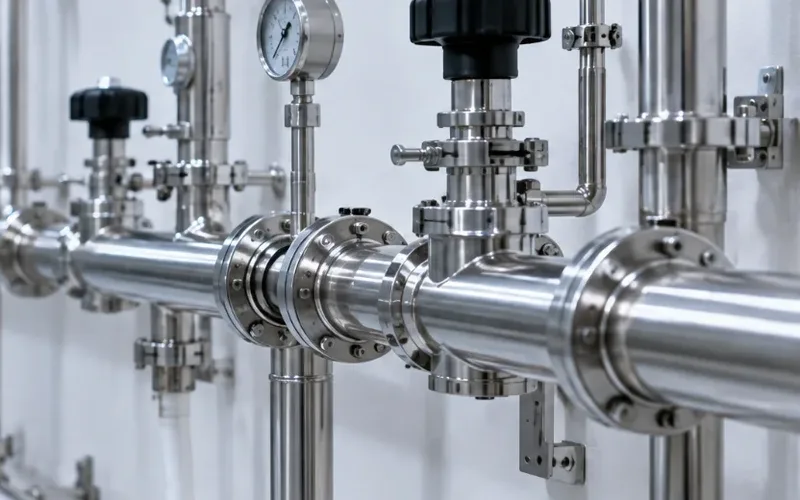
Every wetted surface stainless, joints included. When corrosive, high-purity or copper-free food liquids rule out copper and nickel braze, this is the plate pack.
+ Learn More
Brazed Plate
Refrigeration
For chillers and industrial refrigeration the braze follows the refrigerant: copper for HFC and HFO, nickel for ammonia, high-pressure plates for CO2.
+ Learn More
Brazed Plate
Hydronics
Commercial hydronic duty is clean water against clean water at modest temperature, a fit for a brazed 316L plate once the braze and the potable code are settled.
+ Learn More